
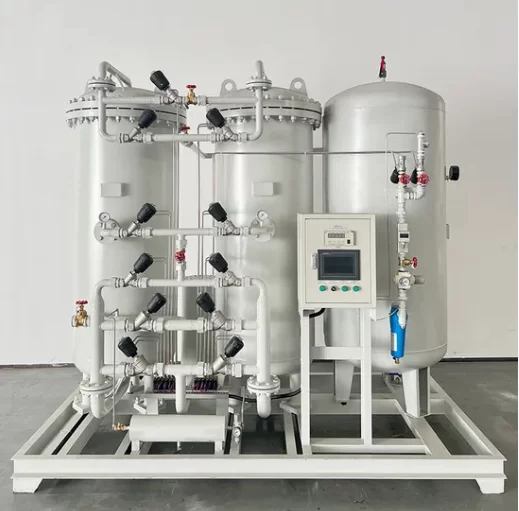

We manufacture high-performance nitrogen separators and generators for industrial and commercial applications worldwide, offering energy-efficient, reliable, and customizable solutions.
As a leading nitrogen separator and generator manufacturer, we provide advanced on-site nitrogen generation systems that deliver consistent, high-purity nitrogen for industries including food and beverage, electronics, metallurgy, chemicals, and pharmaceuticals. Our expertise focuses on designing and manufacturing Pressure Swing Adsorption (PSA) and Membrane Nitrogen Generators to meet the most demanding requirements for purity, flow rate, and operational efficiency.
Backed by years of engineering experience and a commitment to innovation, we offer factory-direct solutions that help customers reduce operating costs, eliminate dependence on bottled nitrogen, and support sustainable production. From standard systems to fully customized projects, we serve customers worldwide with ISO-certified manufacturing quality and professional technical support.
Professional Manufacturer Expertise
Years of experience in nitrogen generation technology, with a proven track record across global industrial projects.
Factory-Direct Supply
Competitive pricing without intermediaries, ensuring cost savings and fast delivery for international customers.
High Purity & Efficiency
Systems capable of producing nitrogen with purity up to 99.999% [reference/typical], optimized for continuous industrial operation.
Customizable Solutions
Tailored to specific customer requirements, including flow rate, purity level, and available space constraints.
Global Technical Support
Comprehensive after-sales services, including installation guidance, remote monitoring, and maintenance planning.
PSA and Membrane Technology: Advanced separation systems using premium carbon molecular sieves (CMS) or membrane modules for efficient nitrogen production.
Smart Control Panel: PLC-based touch-screen interface for convenient monitoring and adjustment of purity and flow settings.
Energy-Efficient Operation: Low power consumption design and variable flow optimization to reduce operating costs.
Industrial-Grade Construction: Durable materials and robust design to support long service life, even in harsh operating environments.
Adjustable Flow & Purity: Flexible configurations to meet requirements across diverse applications, from food packaging to electronics manufacturing.
Integrated Safety Systems: Built-in alarms for pressure, purity, and system performance to support safe and reliable operation.
Compact & Modular Design: Space-saving configuration with scalable capacity to support future expansion.
Product Details
Customization: | Available |
Application Fields: | Medical |
Certification: | ISO |
Model NO. | QTN39 nitrogen generator | Condition | New |
Noise Level | Low | Parts | Transformers |
Purpose | Gas Separation | Nitrogen Flow Rate | 5~5000 nm/h |
Nitrogen Purity | 95~99.9995% | Nitrogen Pressure | 0~0.8 MPa (Adjustable) |
Dew Point | -40°C~-60°C (Atm. Pressure) | Usage | Hydrogen, Nitrogen, Oxygen |
Machine Size | Small | Transport Package | Wooden Box |
Specification | 1–1000 cubic meters | Trademark | Lixin Zhexing |
Origin | Hebeihengshui | HS Code | 8419601900 |
Production Capacity | 100 sets/Year |
Product Description
Technical characteristics
1. The equipment features low energy consumption, low cost, strong adaptability, fast gas production, and easy purity adjustment.
2. Modular structural design saves floor space.
3. Easy to operate, stable performance, high automation level, and capable of unmanned operation.
4. Reasonable internal structure design improves the adsorption efficiency of zeolite molecular sieves.
5. Special airflow diffusion settings reduce the impact of high-speed airflow and extend the service life of zeolite molecular sieves.
6. The use of well-known brands for key components provides effective assurance of equipment quality.
7. Automatic interlocking venting device to ensure the quality of produced nitrogen.
8. Optional features including touch-screen display, dew point detection, energy-saving control, DCS communication, etc.