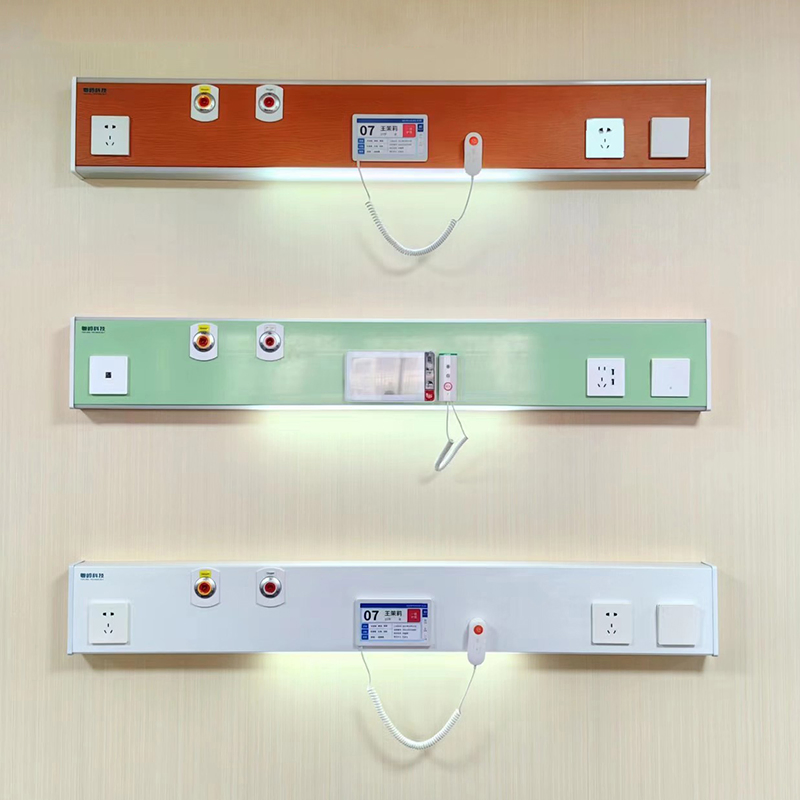
As a manufacturer of medical equipment belts, we design and produce durable, ergonomic belts for medical and hospital applications.
Our product range includes patient transfer belts, restraint belts, surgical support belts, and customizable straps for hospital equipment. Designed with both patients and healthcare professionals in mind, these belts help ensure safety, comfort, and reliable performance in daily hospital operations.
Each belt is manufactured using medical-grade materials that comply with international health and safety standards. Whether for patient mobility assistance, surgical support, or securing medical equipment, our belts deliver optimal performance and long-lasting durability—making them an essential accessory for modern healthcare facilities.
Specialized Manufacturing Expertise
With years of experience in the medical sector, we develop belts tailored to a wide range of clinical and hospital scenarios.
Compliance with Global Standards
All products are designed and manufactured in line with ISO, FDA, and CE frameworks to support safety and reliability.
Customizable Solutions
We offer a wide range of belt sizes, materials, colors, and configurations to meet specific customer requirements. OEM and ODM services are available.
Durable and Comfortable Design
Our belts are made from high-strength, hypoallergenic materials to maximize patient comfort and ensure easy handling for caregivers.
Competitive Pricing and Scalable Production
Our advanced production facilities enable us to deliver high-quality products at competitive prices, with dependable lead times.
Medical-Grade Materials: Made from antibacterial, breathable, and hypoallergenic fabrics for safe patient use.
Ergonomic Design: Engineered for maximum comfort and ease of use, helping reduce strain for both patients and healthcare staff.
Secure Fastening Systems: Heavy-duty buckles, Velcro, or magnetic closures for a secure, adjustable fit.
Wide Application: Suitable for patient transfer, mobility support, rehabilitation, surgical positioning, and equipment fastening in hospitals and clinics.
Custom Branding Available: Logos, colors, and packaging can be tailored to meet customer specifications for OEM/ODM orders.
High Strength and Durability: Resistant to repeated washing and sterilization for long-term use in medical environments.
Product Details
Customization: |
Available |
Warranty: |
1 Year |
Certification: |
ISO9001, CE, ISO, CE |
|
Model NO. |
Medical gas engineering |
Noise Level |
Low |
|
|
Voltage |
220V |
Purity |
93.5%-94.5% |
|
|
Usage |
Oxygen |
Parts |
Valve |
|
|
Application Fields |
Medical |
Machine Size |
Large |
|
|
Condition |
New |
Purpose |
Medical Center Oxygen Supply |
|
|
Does It Support Processing |
Yes |
Product Type |
Compressed Oxygen Production |
|
|
Applicable Scope |
Hospitals, Nursing Homes, etc |
Install |
Can Be Installed on Site |
|
|
Characteristic |
Stable Performance |
Transport Package |
Wooden Box |
|
|
Specification |
Wooden box |
Trademark |
Lixin Zhexing |
|
|
Origin |
Hengshui, Hebei |
HS Code |
8419601900 |
|
|
Production Capacity |
5000 Square Meters |
Product Description
The medical center gas supply system is an essential component of modern hospitals. It includes oxygen, vacuum suction, compressed air, laughing gas, nitrogen, carbon dioxide, and more.
The medical center gas supply system consists of a central gas supply station, pipelines, valves, pressure-monitoring devices, flow meters (specifically for oxygen), alarm devices, and gas terminals. Medical gases are delivered to terminals in operating rooms, emergency rooms, treatment rooms, and various wards through pressure-stabilizing devices, pipelines, valves, and related components for medical use.
How a Professional Manufacturer of Medical Equipment Belts/Hospital Equipment Belts Ensures Quality and Compliance
A professional manufacturer of medical equipment belts/hospital equipment belts plays a critical role in ensuring that healthcare facilities receive products that meet strict safety, performance, and regulatory requirements. Quality and compliance form the foundation of medical device production. Trusted manufacturers operate under well-defined standards and verification systems to support the reliability of every belt used in hospitals, clinics, and emergency care units.
First, a certified manufacturer follows internationally recognized medical-grade standards such as ISO 13485, FDA guidelines, and applicable CE compliance frameworks. These certifications help ensure that product design, material selection, production methods, and factory management follow strict medical device industry requirements. Materials used for medical equipment belts/hospital equipment belts must be durable, hypoallergenic, and resistant to sterilization treatments to support both patient comfort and long-term operational performance.
In addition, quality assurance is implemented at every stage of the production cycle—from raw material procurement to final packaging. Modern factories use automated cutting, stitching, and bonding technologies to maintain precision and reduce the risk of human error. Final inspection teams conduct tensile strength tests, wear-resistance tests, fastening performance checks, and surface safety assessments to help ensure that no defective products enter the medical supply chain.
Furthermore, traceability is essential for compliance. Each batch of belts is assigned a unique tracking code for documentation, recall control, and performance monitoring. This traceability enables hospitals and distributors to maintain detailed records and supports accountability throughout the supply chain.
Continuous R&D is another key element of compliance. A professional manufacturer invests in research to optimize ergonomic design, enhance breathable performance, improve safety locking systems, and update materials in line with evolving healthcare standards. Collaboration with medical professionals helps align new product developments with real clinical needs.
Ultimately, compliance is not only about meeting regulations—it is about protecting patients and supporting healthcare staff. By combining standardized production, rigorous certification, controlled documentation, and continuous innovation, a professional manufacturer helps maintain global confidence in medical products and contributes to safe, efficient operation across modern healthcare systems.
The Role of a Professional Manufacturer of Medical Equipment Belts/Hospital Equipment Belts in Modern Healthcare
In modern healthcare systems, a professional manufacturer of medical equipment belts/hospital equipment belts plays an indispensable role in supporting patient mobility, surgical procedures, rehabilitation, emergency transport, and overall hospital workflow efficiency. Although medical belts may appear to be simple accessories, they are important components across many clinical settings—helping to ensure patient stability, safety, and comfort during care.
One primary role is patient support. Transfer belts used in elderly care and rehabilitation centers, restraint belts used during surgical procedures, and abdominal and orthopedic belts used in postoperative recovery all demonstrate diverse applications that directly influence patient outcomes. Without reliable and ergonomically designed belts, medical staff may face greater difficulty in supporting the safe mobility of patients with limited movement or stabilizing individuals during treatment.
Another critical role is operational efficiency. Hospitals rely on standardized medical supplies that are compatible with equipment, easy to clean, and suitable for repeated use. A professional manufacturer ensures that belts meet these requirements, helping reduce replacement frequency related to wear and supporting cost control without compromising safety.
Professional manufacturers also support innovation in medical technology. They collaborate with surgeons, physiotherapists, and rehabilitation experts to develop new designs that address emerging clinical needs. For example, belts with enhanced ventilation layers improve wearer comfort during extended recovery, while quick-release locking mechanisms improve response time in emergency scenarios.
Global healthcare requirements also demand specialized customization. A professional manufacturer can produce belts tailored for neonatal care, bariatric use, emergency ambulance stretchers, or ICU restraint systems. This flexibility helps hospitals procure products that align with patient categories, regulatory guidelines, and equipment compatibility standards.
In addition, as populations age and chronic disease care increases, demand for reliable mobility support equipment continues to grow. Manufacturers help ensure that medical belts remain safe for long-term use, reducing caregiver injury risks and supporting patient independence.
Ultimately, the presence of a professional manufacturer of medical equipment belts/hospital equipment belts helps hospitals, clinics, elderly care centers, and rehabilitation institutions operate smoothly. Their contributions extend far beyond production—they help shape global care standards, strengthen safety, and support clinical professionals in delivering high-quality treatment to patients worldwide.
Future Market Trends for a Professional Manufacturer of Medical Equipment Belts/Hospital Equipment Belts
The global medical infrastructure industry continues to expand rapidly, and the future holds promising opportunities for a professional manufacturer of medical equipment belts/hospital equipment belts as healthcare systems evolve. Demographic changes, hospital construction growth, regulatory upgrades, and technology integration are all shaping this specialized medical terminal equipment sector.
One of the strongest market drivers is the ongoing increase in global healthcare investment, particularly for hospital infrastructure upgrades. Medical equipment belts—commonly installed at the head of hospital beds—serve as essential multifunctional terminal systems that support oxygen supply, negative pressure suction, medical gas outlets, lighting, nurse call systems, and electrical interfaces. As governments, private healthcare groups, and rehabilitation facilities expand capacity, demand for structured, standardized, and safety-certified headwall equipment belts is expected to continue increasing.
Customization and ergonomic installation are becoming major trends. Modern hospitals require flexible configurations aligned with department needs, including ICU, emergency wards, general wards, maternity wards, and rehabilitation rooms. Future medical equipment belts are expected to support modular design, selective gas terminal layouts, anti-bacterial surface treatments, LED lighting options, smart call systems, and aesthetic integration that matches interior design standards. Manufacturers capable of OEM/ODM customization, engineering support, and on-site integration will gain stronger competitiveness in global tendering environments.
Technology integration will also accelerate sector transformation. Smart hospital concepts are driving the adoption of IoT-enabled patient monitoring systems, digital nurse-call communication, real-time diagnostic feedback, and intelligent lighting controls integrated into equipment belts. These innovations improve hospital workflow efficiency, reduce medical errors, and enhance patient comfort—supporting the direction of digital healthcare ecosystems.
Sustainability trends are gaining importance, particularly in emerging procurement requirements. Medical facilities increasingly seek durable aluminum structures, recyclable materials, low-energy lighting systems, safe electrical insulation, and maintenance-friendly modular components to extend product lifecycle and reduce total operating costs. Manufacturers that embrace sustainable materials and precision manufacturing will be better positioned to meet international quality expectations.
From a regulatory perspective, global medical compliance frameworks continue to tighten. Manufacturers need to invest in quality assurance systems, electrical safety testing, gas terminal certification, installation standards, documentation management, and international certification compliance. Strong conformity in ISO, CE, electrical safety standards, and medical gas requirements will be increasingly important for entry into international markets and government procurement programs.
Geographically, emerging markets such as Southeast Asia, Latin America, Eastern Europe, and the Middle East are undergoing large-scale hospital construction and modernization. This creates strong procurement demand for integrated medical equipment belt systems. A professional manufacturer of medical equipment belts/hospital equipment belts with international logistics capability, on-site installation guidance, and multilingual communication support will be well positioned for long-term global expansion.
In conclusion, the future market outlook favors companies that embrace technological innovation, modular engineering solutions, international compliance, and sustainable production. Manufacturers that adapt to evolving hospital needs and global healthcare modernization will lead the next phase of industry growth and contribute to improved medical safety, efficiency, and patient experience worldwide.